Rear spoiler brackets need secure attachments and a controlled exterior finish. This application concept combines robot positioning, a pneumatic ultrasonic welding module and dedicated fixtures for compatible thermoplastic brackets and internal supports with suitable overlapping joining areas.
The illustrated layout supports a review of tool access, local support and the joining sequence. Final equipment and settings depend on the actual parts and production requirements.
|
Application item |
Proposed solution |
|
Component |
Molded rear spoiler with thermoplastic brackets or internal supports. |
|
Joining locations |
Accessible overlapping attachment areas on the reverse side. |
|
Welding module |
Pneumatic actuation, guided motion and a slim flat piercing horn. |
|
Cell concept |
Robot positioning with dedicated fixtures; one robot and two fixtures are illustrated. |
|
Project release |
Material compatibility, joint strength, appearance and the full station cycle verified on actual parts. |
Dizo Sonics can evaluate this arrangement using its robotic ultrasonic welding workstation. Robot reach, horn clearance, fixture support and the required station cycle determine the proposed equipment configuration.
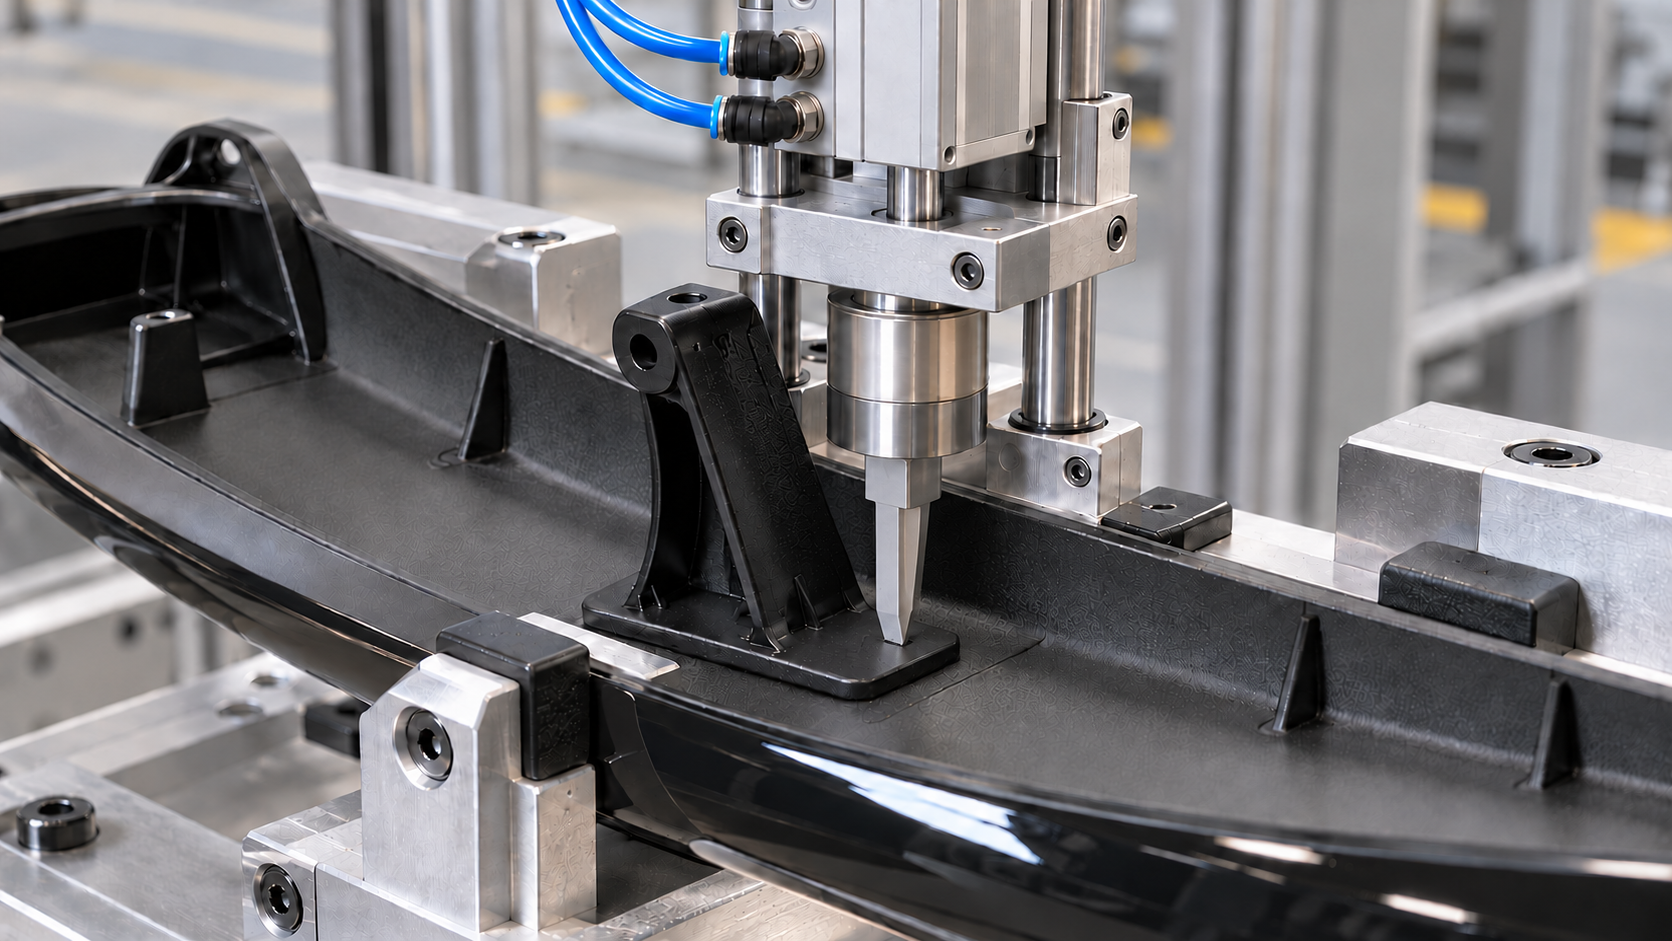
The robot places the tool at each joining location. The pneumatic axis provides approach and pressing motion, while the guide maintains alignment. The generator and acoustic stack deliver ultrasonic vibration through a slim flat piercing horn to the overlapping plastic attachment area. The horn penetration, ultrasonic settings and hold conditions are established through trials on production-intent parts.
AI-generated application illustration: pneumatic actuation, guidance and a slim flat piercing horn at a bracket attachment point. Final horn geometry requires part trials.
Ultrasonic spot welding can form a local joint through overlapping thermoplastic components. Herrmann describes spot welding and other ultrasonic joint types. Suitability depends on the actual resin grades, overlap geometry, component thickness and support beneath the joining point.
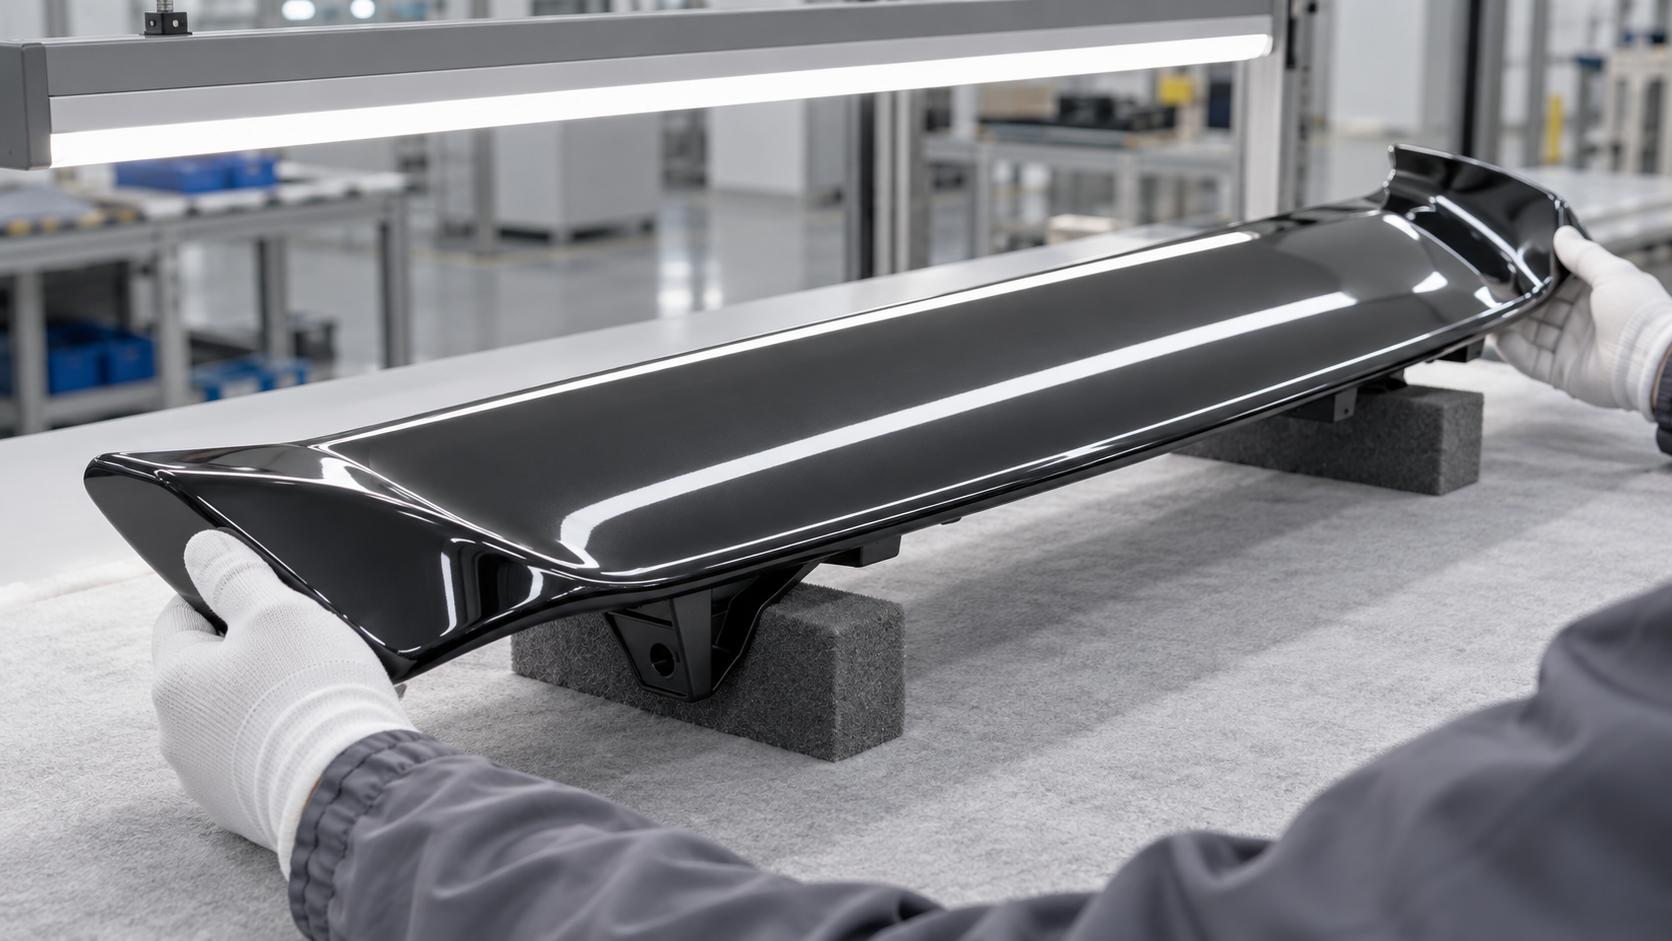
The nest should support the joining areas and protect the visible side. Select contact surfaces and clamps for the actual part geometry and finish. Inspect appearance after welding and fixture release under defined lighting and viewing conditions.
AI-generated application illustration of rear spoiler surface inspection under linear lighting.
|
Check |
Acceptance basis |
|
Bracket retention |
Specified load direction, test method and required retention. |
|
Location and fit |
Bracket position and completed assembly fit against the drawing. |
|
Visible surface |
Customer criteria for marks, whitening, distortion and print-through. |
|
Repeatability |
Agreed sampling across joining points, variants and start or restart conditions. |
|
Conditioned performance |
Exposure and retesting where required by the customer specification. |
Set limits from the approved drawing and customer specification. Confirm cycle records with physical checks on the completed assembly.
Send the 3D model, joining map, material grades, samples, finish requirements, retention test and target station cycle. Contact Dizo Sonics to review robotic ultrasonic welding for your rear spoiler assembly.

